Top 3D Printer Resin Supplier Guide for High-Quality Prints
2026-10-16
Finding a resin supplier that consistently delivers high-quality prints is harder than most people expect. You can dial in exposure settings and support placement perfectly, yet a single bad batch of resin still ruins the entire job. That is why we put together this guide to the top 3D printer resin suppliers, with a closer look at ProtoMat and what sets their materials apart for demanding print work. Whether you are chasing fine detail on miniatures or need durable functional parts, the right resin partner changes everything.
What Sets a Dependable Resin Supplier Apart
A dependable resin supplier stands out through a quiet consistency that shows up in every batch. Rather than leaving you to discover viscosity shifts or unexpected gel-time changes on the production floor, they test each lot before dispatch and include a concise certificate of analysis with key parameters like epoxy equivalent weight, viscosity, and cured hardness. This habit of sharing data proactively, without waiting for a customer to ask, cuts down the trial-and-error that eats into production schedules.
Technical response is another differentiator. When a cure comes out tacky, color drifts, or surface defects appear, you need to reach someone who understands resin chemistry and real-world molding or coating processes, not a call-center handoff. Dependable suppliers typically have engineers who will look at your process parameters, examine samples, or even join a video call to pinpoint whether the issue stems from material variation or a shift in shop conditions. That level of involvement prevents small hiccups from becoming costly downtime.
Supply-chain transparency also separates the dependable from the merely available. A supplier worth keeping will flag raw-material lead-time risks before they hit, offer a realistic buffer when price adjustments are unavoidable, and provide pilot samples of any alternative resin so you can validate performance on your own line. They don't hide differences between standard and substitute products; instead, they give you the data and time to switch over without disrupting your output.
Cracking the Code on Resin Technical Data
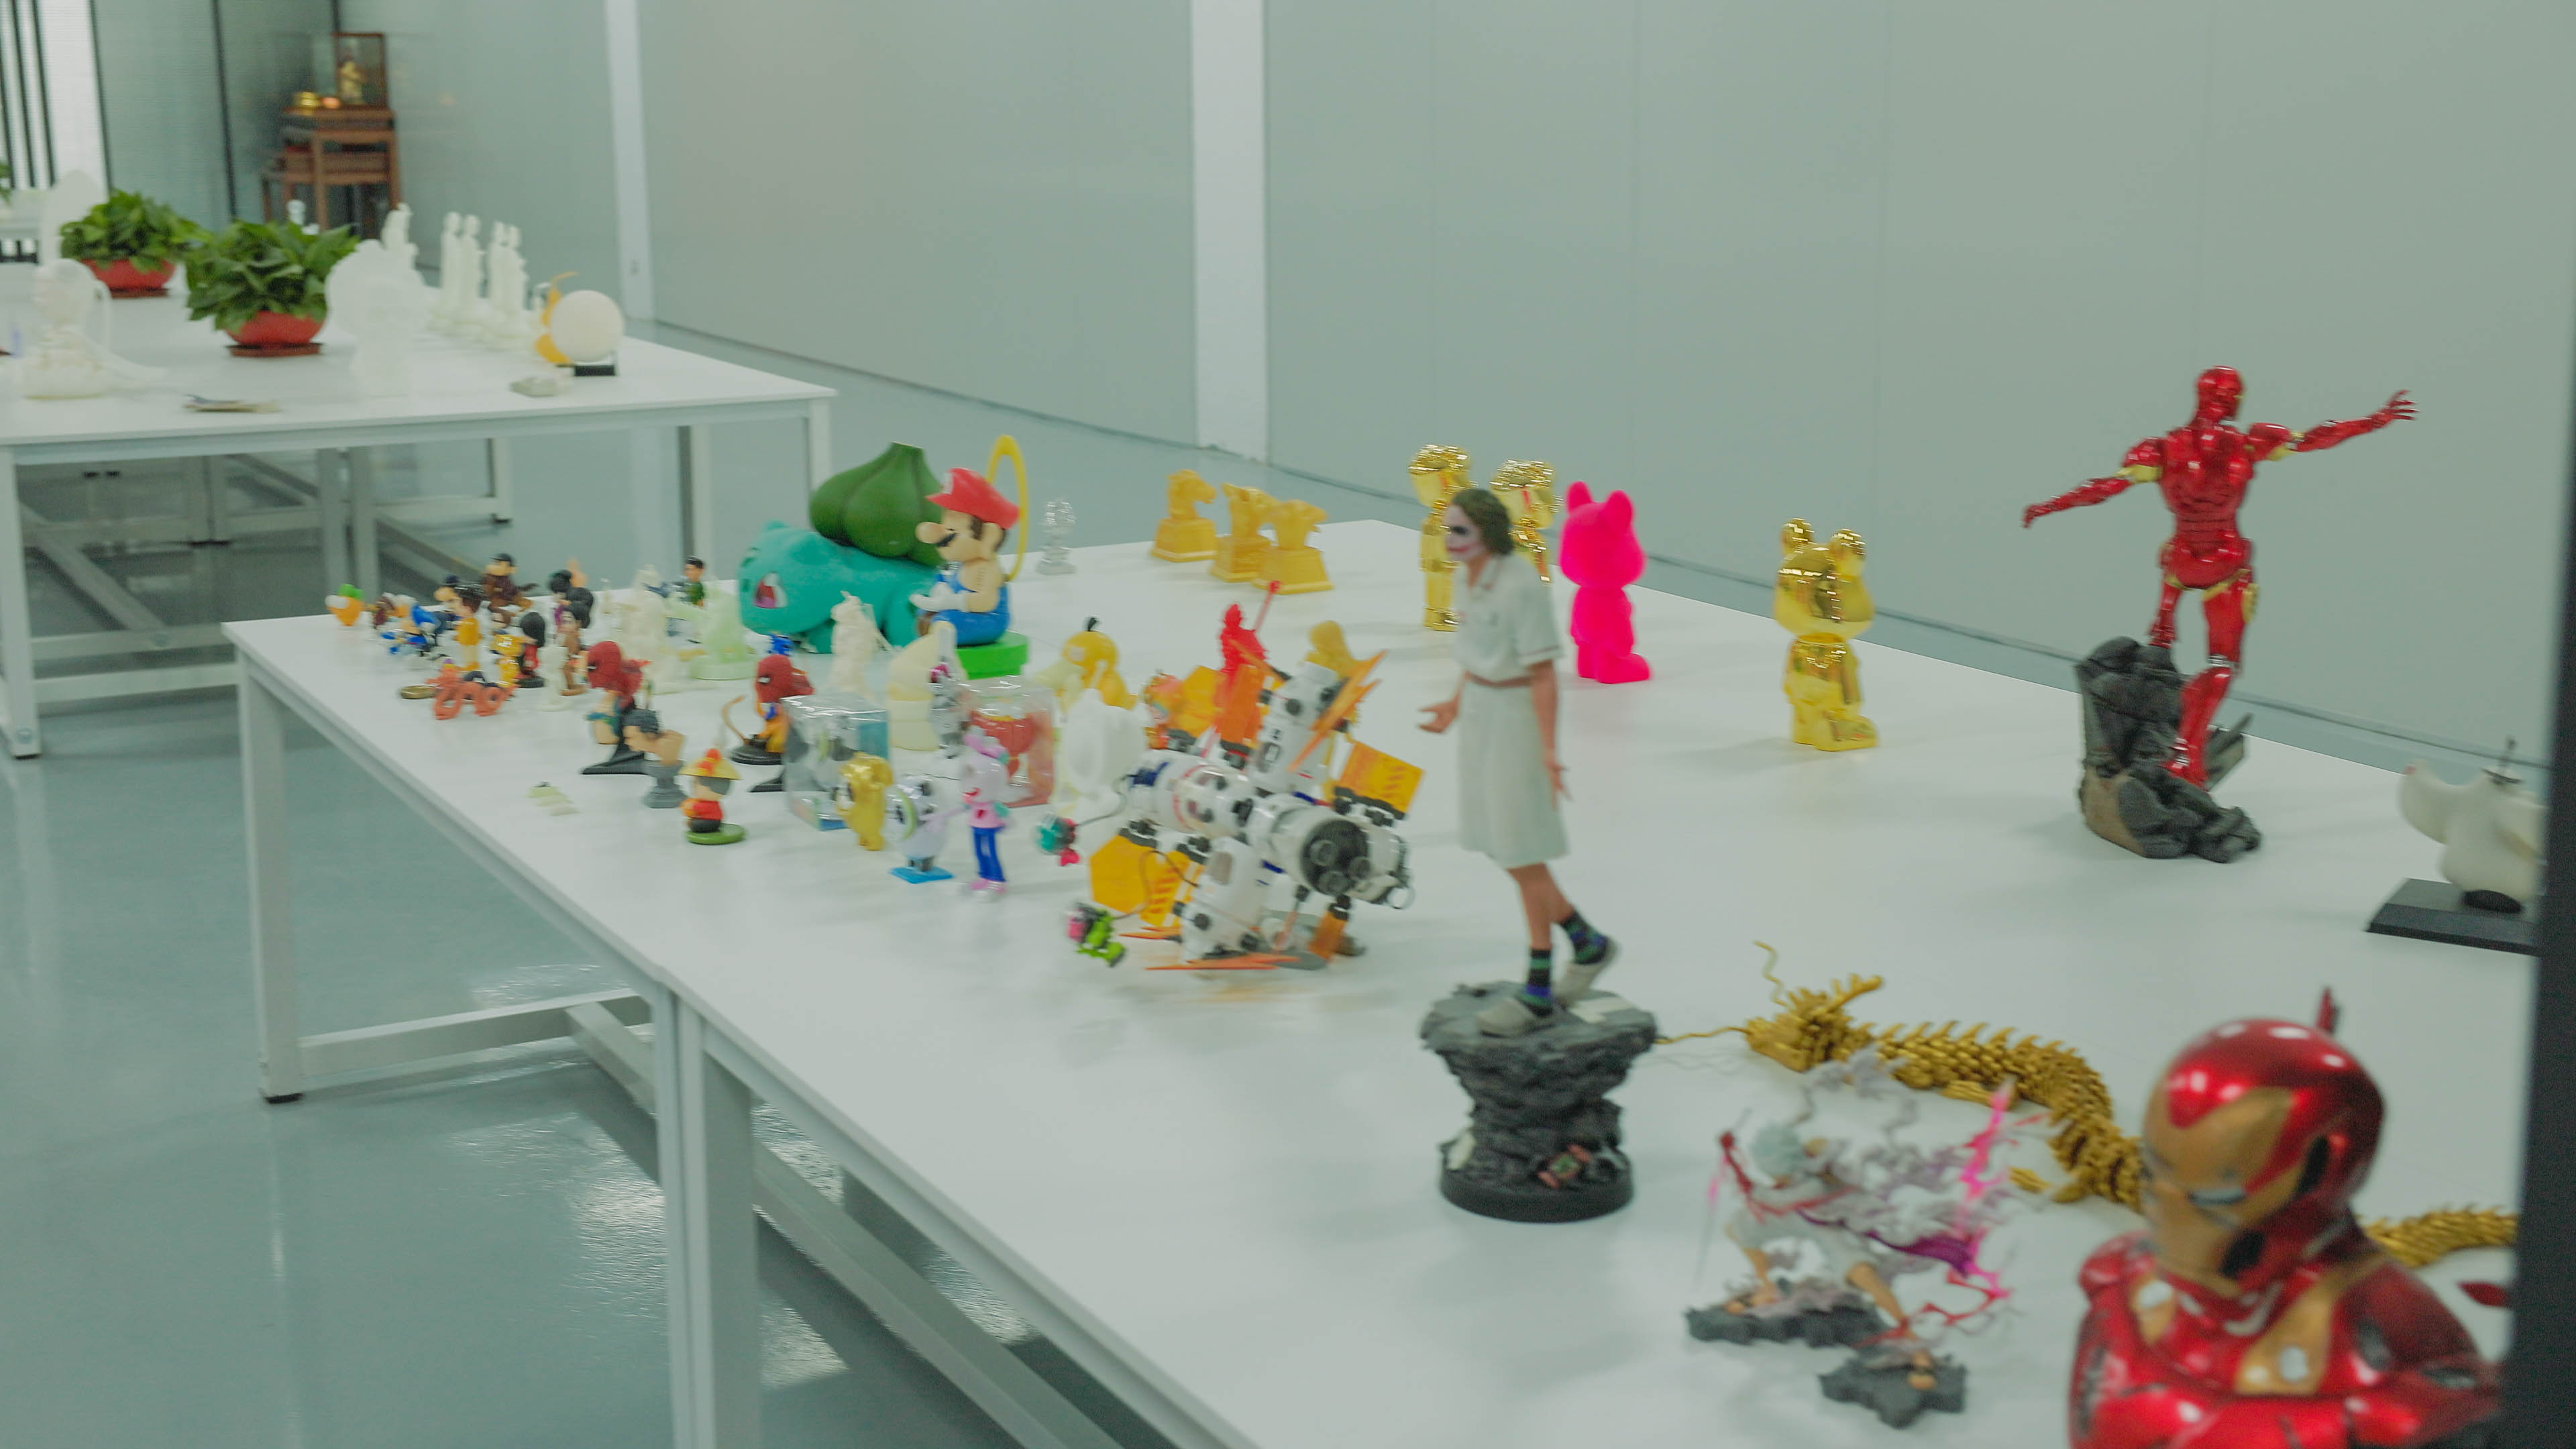
Resin datasheets tend to bury the numbers that actually matter for your process. A high tensile strength on paper doesn't tell you how the material will behave when your print is under repeated load or exposed to moisture. Start with the viscosity curve, not the single value at 25°C; how it changes between 20°C and 30°C is what determines whether you'll get consistent layer curing or a clogged vat.
Look for the gap between flexural modulus and elongation at break. A resin can be stiff but crack-prone if elongation is under 4%, even when its modulus looks impressive. Also keep an eye on water absorption after 24 hours—many datasheets hide this in fine print, but a 2% uptake can warp thin walls and kill dimensional accuracy long before mechanical failure shows up.
Finally, treat the cure depth and exposure times as a starting range, not a fixed recipe. Your printer's light source, film thickness, and even ambient temperature shift those numbers. The real skill is learning to read between the lines: compare values at the same test method (ISO vs ASTM often don't mix), and always ask for the full curve, not just the headline figure.
Resin Types That Deliver Detail Without the Drama
If you want prints with razor-sharp edges but dread the brittle snap of standard resins, ABS-like formulations are worth a closer look. They hold the same fine surface detail as traditional gray resins, yet they flex just enough to survive support removal and the occasional drop from a workbench. That blend of precision and forgiveness makes them a quiet favorite for miniature painters and product designers who need functional prototypes without a padded shipping box.
Water-washable resins offer another low-friction route to crisp results. No IPA bath, no sticky residue after cleaning, just a rinse under the tap and the details stay tight on filigree, facial features, and mechanical joints. For anyone working in a shared space, low-odor plant-based options have also matured: the best ones now print with clean layer lines and minimal warping, so you are not trading surface quality for a friendlier smell.
Supplier Vetting Questions Worth Asking Early
Most sourcing teams wait until a supplier is already in the pipeline before digging into operational details. Then surprises surface late: a factory running at 110% capacity, a sub-tier partner with no traceability, or a quality lab that only exists on paper. Early vetting flips that pattern. Instead of asking “Can you make this?” the first questions should be “Who actually makes it, and how do you prove consistency?”
Three areas deserve blunt inquiry before any sample request. First, ask for a live production schedule, not a capacity statement. If a supplier cannot show which lines are committed and which are open by week, their promise of “no problem” means little. Second, ask for the name and location of the last three shipments that failed inspection. Every factory has failures; the ones worth working with can walk you through root cause and corrective action without getting defensive. Third, ask who owns the tooling and what happens to it if the relationship ends. That single question often exposes whether you’re dealing with a partner or a middleman.
Finally, test the supplier’s questions about you. A capable manufacturer will ask about forecast variance, packaging constraints, and tolerance for defect rates before quoting a price. If their only question is “How many units?” they have not thought about your production reality. Early vetting is not a checklist to complete; it’s a conversation to see how the supplier thinks under mild pressure.
Why Batch Consistency Matters More Than You Think
Most people assume that if a product worked well once, it will work the same way every time. But batch consistency quietly decides whether that trust survives. A supplement with slightly different particle sizes, a ceramic glaze mixed at a different humidity, a sauce fermented two hours longer—these aren't abstract variables. They're where customer loyalty is won or lost, often before anyone files a complaint.
The real danger isn't a dramatic failure. It's the slow drift that makes your product feel unpredictable. One batch dissolves faster, another clumps, a third has a shade that's almost right. Your repeat buyers notice. They may not be able to articulate the difference, but they stop reordering. Consistency isn't a quality control checkbox; it's the baseline condition for building habits around your product.
What makes this harder is that consistency demands discipline in the unglamorous parts of production: raw material sourcing, mixing times, temperature logs, even how long materials sit before processing. When you ignore those details, you're not just risking a bad batch. You're teaching your market that your product can't be relied on, and that's a lesson they'll remember long after you've fixed the recipe.
Testing New Resins Without Wasting a Full Bottle
You don't need to pour an entire bottle just to see if a resin works for your project. Start with a small batch, around ten to fifteen milliliters, mixed in a disposable cup. This gives you enough material to coat a test swatch or cast a thin layer, and you can observe how it levels, cures, and releases from the mold before committing to a larger pour.
A clever trick is to use a digital scale to measure the resin and hardener by weight instead of volume. That way you can mix as little as five grams total without losing accuracy. Keep notes on the exact ratio and ambient temperature, because some resins behave differently in small masses—they might cure slower or trap fewer bubbles than a deep pour would.
If you often test new formulas, keep a set of tiny silicone molds or flat plastic sheets ready. A single drop on a sheet shows you the cured clarity and surface finish, while a few grams in a small cavity reveals shrinkage or warping. This approach saves both money and frustration, letting you screen out bad candidates before you open a second bottle.
FAQ
Look for suppliers that publish detailed technical data sheets, including viscosity, tensile strength, and shrinkage rates. Consistency matters more than a single perfect batch—ask about their batch-to-batch variation testing. A reliable supplier will also provide clear storage and handling guidelines, and they usually have a responsive support team if problems arise during printing.
Lower viscosity tends to help resin flow back into the vat quickly, reducing layer lines and improving fine detail. Low shrinkage is also critical—if the resin contracts significantly during curing, you will see warping and dimensional inaccuracy. Pigment load and photoinitiator concentration matter too, as they affect exposure times and cure depth. So a balanced formulation designed for high resolution is what you are after.
Yes. For miniatures and display pieces, look for high-detail resins with high pigment load and low shrinkage—they capture sharp edges and fine textures. For functional parts, engineering resins that offer higher impact resistance, flexibility, or temperature tolerance are better, even if they sacrifice a little surface crispness. Some suppliers offer specialty resins like castable or flexible options for niche applications.
Going straight for the cheapest option is the biggest trap. Cheap resins often have inconsistent viscosity and higher shrinkage, leading to failed prints and wasted time. Another mistake is ignoring the recommended exposure settings for your specific printer—using generic settings can cause over- or under-curing. Also, some people skip reading the safety data sheet and then deal with skin irritation or ventilation problems.
Start with a small sample bottle—many suppliers offer 250ml or 500ml sizes. Print a calibration model that includes fine text, sharp edges, overhangs, and small holes. Run it at the recommended settings, then inspect for detail retention, dimensional accuracy, and surface quality. Also test post-curing behavior: some resins get brittle or yellow if over-cured. If the sample performs well across several prints, you can safely order a larger batch.
Absolutely. For DLP and MSLA printers with a monochrome screen, a lower viscosity resin drains back faster between layers, which reduces print time and ghosting artifacts. For SLA printers with a wiper or flexible vat, you can get away with slightly higher viscosity, but too thick a resin can still cause layer separation. Check the supplier's viscosity spec and compare it to your printer manufacturer's recommendations.
Resin is temperature-sensitive. Most formulations perform best between 20°C and 30°C—colder resin gets viscous and underexposes, while hot resin can over-cure and lose detail. Store bottles in a cool, dark place, away from UV light and moisture. Always shake or stir the resin before pouring, because pigments and photoinitiators can settle. If your print room is cold, consider a heated enclosure or warming the resin bottle in warm water before printing.
Look for a supplier that publishes detailed printing profiles for popular machines, offers troubleshooting guides, and has real technical support—not just a sales team. Some suppliers provide exposure test files or recommended post-processing steps. A good supplier also discloses the resin's safety and disposal requirements clearly. If a supplier is opaque about their formulation or cannot answer technical questions, that is a red flag.
Conclusion
Finding a resin supplier that consistently delivers high-quality prints isn't about chasing the lowest price or the flashiest label. It starts with suppliers who openly share batch-specific technical data sheets, not just generic marketing spec sheets. You want a partner who can tell you the exact exposure settings, viscosity range, and pigment stability for the lot you're ordering today. That level of transparency separates the professionals from the resellers. Equally important is knowing which resin type fits your workflow: standard resins for crisp prototypes, tough or ABS-like resins for functional parts, and specialty resins for castable or high-temperature applications. A dependable supplier will guide you toward the right chemistry instead of pushing whatever's overstocked.
Before committing, ask pointed questions early: How often do they re-test raw materials? Can they provide samples from the same batch you'll later purchase? Do they track and publish batch-to-batch variance? Consistency here is not a nice-to-have—it's the difference between dialing in settings once and re-calibrating after every order. When testing a new resin, don't waste a full bottle. Run small exposure test prints or a simple calibration matrix first, then scale up once you've locked in the sweet spot. Suppliers worth keeping will support that process with clear starting points and responsive technical help, not deflect with vague answers. Over time, you'll build a shortlist of suppliers who treat resin quality as an engineering discipline, not a commodity lottery.
Contact Us
Contact Person: Joe
Email: [email protected]
Tel/WhatsApp: +8613799507208
Website: https://www.3dprotomat.com/