Top 10 Concrete Reclaimer Systems for Efficient Aggregate Recovery
2026-09-16
Every cubic yard of leftover concrete hides a profitable secret—if you have the right reclaimer. The problem? Too many systems promise efficient aggregate recovery but end up wasting water, energy, and your patience. That's why we dug through the noise and tested the field to bring you a no-nonsense list of the top 10 concrete reclaimers that actually deliver clean sand, gravel, and reusable slurry. Among the standouts, Sinou caught our attention with its rugged build and surprisingly low maintenance. Whether you're running a small batching plant or a large precast operation, the next ten minutes could change how you handle every leftover pour.
Why Sloped Troughs Recover More Fine Sand Than Flat-Bed Alternatives
A sloped trough introduces a continuous downhill flow component that flat-bed systems simply cannot replicate. As slurry travels across the incline, particles of different sizes and densities experience slightly different settling paths. Fine sand, which tends to stay suspended in a horizontal stream, gets drawn into the slower-moving lower layer where it can settle out rather than being carried over the discharge lip. Flat-bed alternatives keep the slurry in a nearly uniform sheet, giving fine grains little chance to escape the main flow.
The slope also changes how the bed behaves. On a flat surface, fine particles can become trapped in a compacted layer or get re-entrained by turbulence. With a properly matched incline, the bed stays loose and mobile, allowing fine sand to migrate downward while lighter material washes away. This continuous stratification, combined with adjustable slope angles for different feed gradations, explains why sloped troughs pull out more fine sand without relying on higher water volumes or extra retention time.
The True Cost of Ignoring Slurry Viscosity in Your Reclaimer
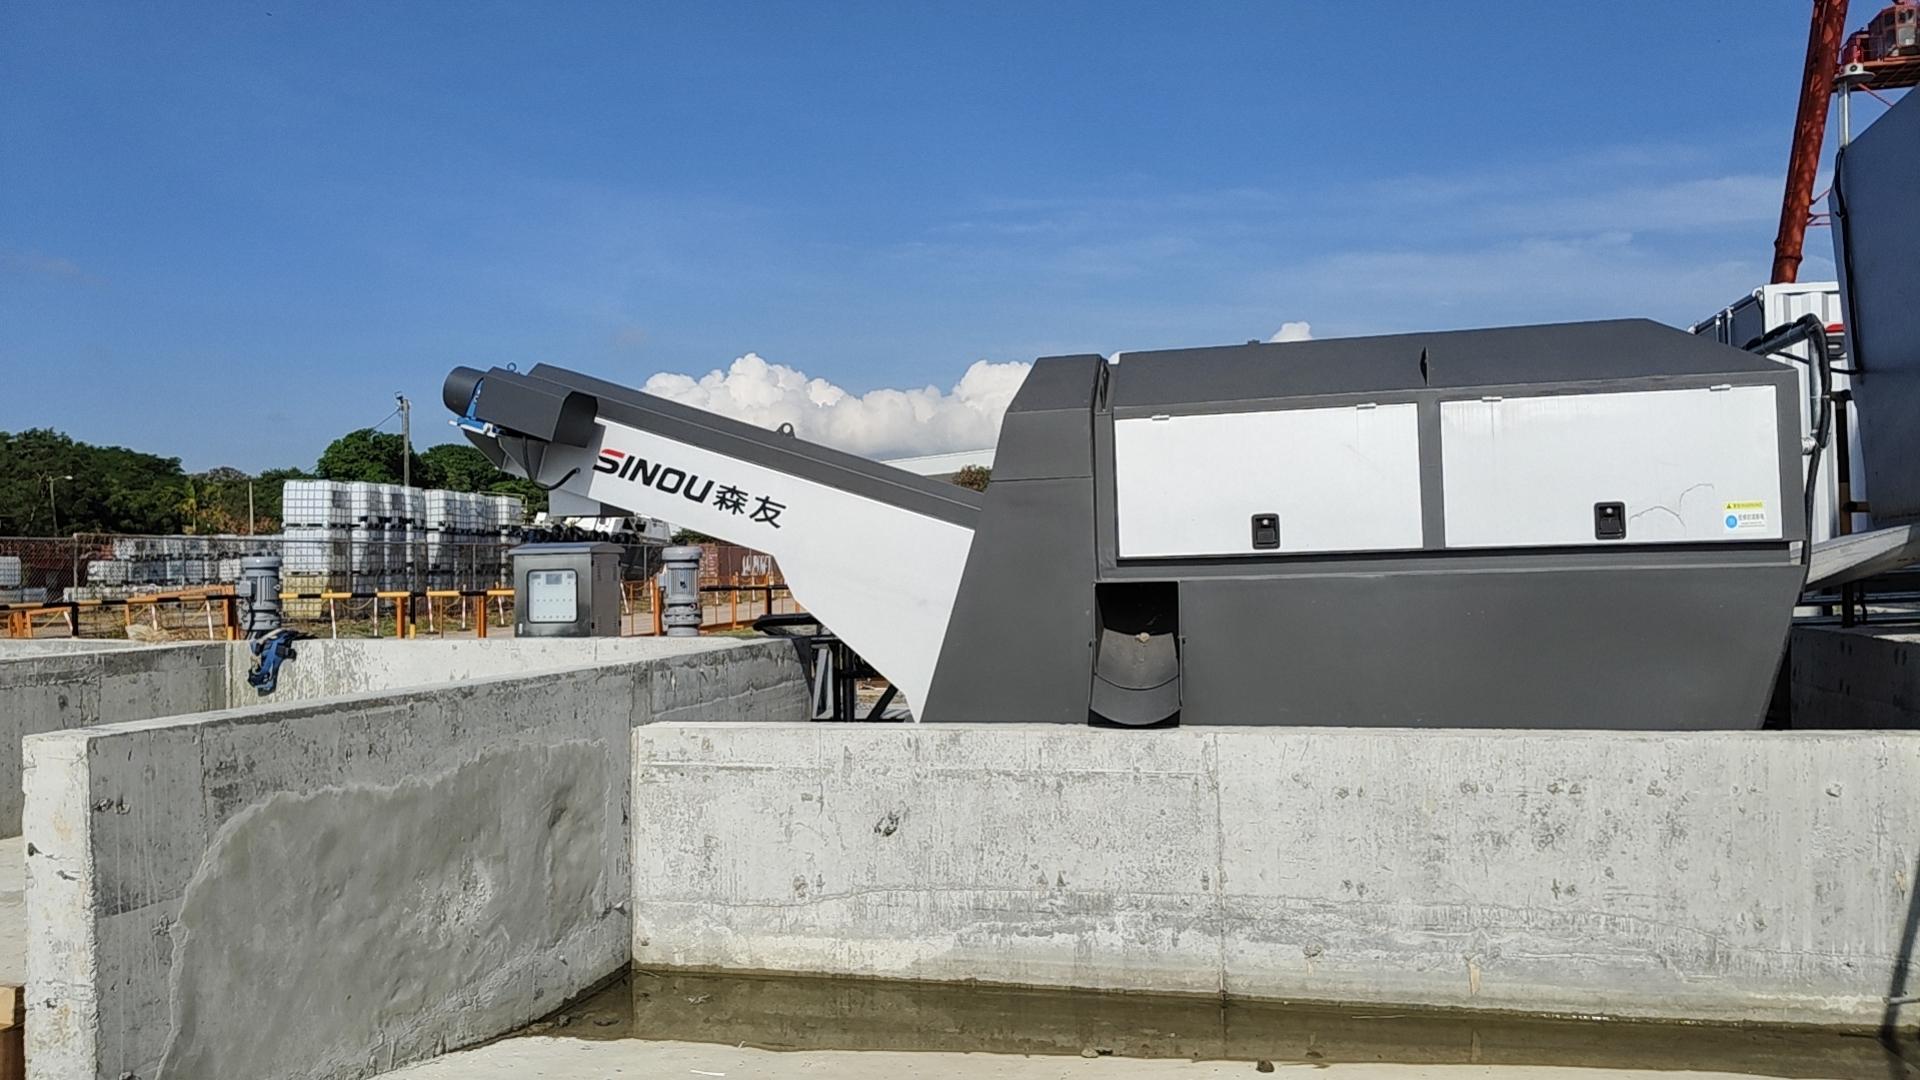
Every reclaimer runs on assumptions, and one of the most dangerous is that slurry viscosity will stay within a predictable window. When it drifts, it rarely announces itself. Instead, you notice the pump sounding labored, the cut taking longer, and the reclaim rate slipping even though nothing about the feed changed. The cost isn't a dramatic failure, it's a quiet tax on every hour of operation.
Ignoring viscosity doesn't just slow you down; it reshapes the entire wear profile of the machine. Thicker slurry forces the impeller and housing to work against higher resistance, generating heat and accelerating erosion in spots that were never meant to bear that load. The result is more frequent rebuilds, unplanned downtime that never shows up in the original budget, and a maintenance log that starts reading like a mystery novel no one wants to finish.
The real cost shows up in the numbers that matter: tons per hour, dollars per ton, and hours between failures. A reclaimer that runs outside its viscosity sweet spot can lose 15 to 30 percent of its throughput without a single alarm going off. Fixing it doesn't require new hardware, just a more honest look at the slurry condition before it enters the machine.
Adjustable Spray Bars: A Simple Change That Boosts Aggregate Yield
Fixed spray bars often run at one angle and one pressure no matter what the feed looks like. When material size, moisture, or clay content shifts, that fixed setting can either blast fine particles off the deck or leave sticky coatings on larger stone. Making the bars adjustable lets operators change spray direction and flow rate in minutes, so the water actually hits the material where it needs to.
The real gain comes from keeping usable fines in the product stream. With adjustable nozzles, you can lower pressure on dry, dusty feed to avoid washing away valuable sand, then raise it on wet, clay-heavy loads to break up mud balls. Some sites also angle the sprays slightly against the material flow, creating a gentle rolling action that lifts contaminants without tossing good aggregate over the side.
In practice, this is often a same-day retrofit. Weld on a slotted bracket or install a threaded manifold, and operators can make adjustments between truckloads instead of waiting for a maintenance crew. Plants that switch to adjustable bars commonly report a few extra tons per shift from the same feed, along with less water use and fewer pile rejections.
Polyurethane vs. Hardox Wear Plates: Which Handles Your Aggregate Type Better?
When your aggregate runs sharp and jagged—think crushed granite or recycled concrete with exposed rebar edges—Hardox wear plate tends to hold its shape longer under heavy gouging. Its hardness spreads point loads, so the surface doesn't tear as quickly. But if you're moving rounded river rock, sand, or softer limestone fines, polyurethane often outlasts steel by letting particles bounce without cutting. The elastic surface absorbs the glancing blows that would normally shave microns off a harder plate.
Wet, sticky material changes the equation again. Polyurethane's low coefficient of friction keeps clay and damp screenings moving instead of building up, while Hardox can pack and stall in chutes. On the flip side, large, high-drop impact zones—like a primary crusher discharge—favor Hardox because polyurethane may flex too much and tear at its mounting holes if the impact is beyond its rebound range. Most operations end up using both: Hardox where the first hit lands, polyurethane where material slides or needs noise dampening.
The grain size matters too. Fine abrasive dust wears polyurethane by erosion, but it doesn't chip or crack the way a hardened steel can under repeated small impacts. For abrasive sands and 3/4-inch minus, polyurethane liners routinely outlast AR400 by two to four times in low-impact zones. For 6-inch plus rock with high velocity, Hardox remains the safer default.
Field-Tested Ways to Extend Reclaimer Service Life Beyond Factory Specs
Most reclaimers die young not from catastrophic failure, but from a thousand small neglects. The factory manual gives you a baseline, yet the machines that outlast their peers by years share a common thread: operators who treat maintenance as a conversation, not a checklist. One field trick is to map wear patterns weekly with a simple paint marker on high-stress zones like the conveyor belt edges and rotor tips. When those marks start disappearing unevenly, you catch misalignment long before vibration sensors complain. Another overlooked habit is logging hydraulic oil temperature swings during the hottest and coldest hours of a shift, not just at startup. That data reveals pump strain that static pressure readings miss.
Beyond routine, the real service-life multiplier lives in how you handle abrasive materials. Instead of accepting the manual’s suggested rotor speed as gospel, seasoned crews often drop it by 5–8% when processing recycled asphalt or high-silica feed. The slightly slower tip speed sacrifices a bit of throughput but cuts impact fracturing on the hammers by nearly half. Pair that with staggered hammer rotation — swapping the outer two rows every 40 hours rather than all at once — and you spread wear so evenly that a set lasts 30% longer. It’s not about babying the machine; it’s about knowing which parts are cheap to run slow and which ones punish you for hesitation.
Finally, stop treating the reclaimer’s undercarriage as an afterthought. Tracks and drive sprockets often fail early because the machine spends its life crawling through milled material that packs into pins and bushings. A five-minute end-of-shift rinse with a low-pressure water wand, focused on the tensioner and idler pockets, prevents that grit from turning into grinding paste overnight. Some operators go further and spray a dry-film graphite lubricant on the track chain every third shift, which repels fine dust without attracting it the way wet grease does. The payoff is not glamorous — just a reclaimer that keeps its tension and alignment through a second or third season, long after the factory warranty has faded into irrelevance.
Batch or Continuous? Matching Reclaimer Type to Your Plant's Daily Pour Volume
A batch reclaimer shines when your daily pour volume swings hard from one shift to the next. You can pre-weigh exact sand-to-binder ratios for each mix, run a limited cycle, and then clean out the drum before the next job. That flexibility matters for plants doing short runs of specialty concrete or frequent color changes, where a continuous unit would leave you flushing material down the drain just to switch recipes.
Once your plant consistently pours above roughly 400 cubic yards a day, a continuous reclaimer starts earning its footprint. Instead of stopping to load and unload, it keeps a steady stream of returned concrete moving through the separation chamber while you keep the trucks rolling. The trick is matching the machine's throughput to your peak return rate, not your average, otherwise you end up with a backlog of waiting mixers and a yard full of half-washed drums.
Plenty of mid-volume plants get stuck trying to force a batch unit to behave like a continuous one, running back-to-back cycles until the operator is too rushed to do proper maintenance. The better move is to log your actual returned concrete over two or three weeks, including those ugly Friday afternoons. Then compare that number against the reclaimer's rated capacity at 80 percent utilization. If you are consistently above that line, continuous is the way. If you dip below it more than twice a week, batch keeps your water and sand cleaner without burning extra horsepower.
FAQ
Look beyond the horsepower and tank size. The real differentiators are wash water pressure, screen mesh options, and how easily the discharge chute can be cleaned. Check whether the unit uses a closed-loop water circuit, because systems that need constant fresh water top-ups will raise your operating costs. Also ask about wear plate thickness on the screw or drum. Thin liners mean early replacement. If possible, request a demo with real returned concrete, not just a controlled slurry, to see how the machine handles lumps and debris.
Most units rely on a combination of mechanical action and water flow. Returned concrete is diluted in a receiving hopper, then passed over a vibrating screen or through a rotating drum. The heavier gravel drops out first while sand and cement fines are carried further by wash water. A screw or wheel then lifts the sand out of the water, leaving cement paste behind. The key is keeping the water velocity high enough to wash the sand but low enough not to carry gravel over the screen.
Concrete production uses a lot of water, and reclaimers return most of it to the batching process. Instead of paying to dispose of alkaline slurry and hauling in fresh water, a closed-loop reclaimer captures the wash water, allows solids to settle, and reuses the grey water in new mixes. This can cut water consumption by 50 to 70 percent. The savings add up fast in areas with strict discharge rules or high water tariffs. Just be sure to monitor the density of the recycled water, since too many fines can affect setting time.
Daily checks matter more than complex overhauls. Clear the spray bars and nozzles because dried concrete will clog them within hours. Grease the screw bearings and check the drive belt tension weekly. Inspect the wear shoes on the screw or drum every month. Once they wear past half their original thickness, replace them before they damage the trough. After each shift, rinse the discharge area and remove any aggregate buildup around the screen. Keep an eye on the water level in the settling tank. Low water leads to cavitation and premature pump failure.
Yes, but it depends on the design. A good reclaimer should accept anything from a dry, zero-slump mix to a soupy, high-slump load without manual adjustment. Look for a variable-speed screw or drum and an automatic water flow control tied to the slurry density. Some units struggle when a dry batch arrives because the material bridges in the hopper. If you regularly get returned concrete with wide slump ranges, choose a system with a high-torque auger and a pre-wash spray ring at the intake to break up lumps before they reach the screen.
Every percent of sand and gravel you recover is material you do not have to buy again. A system that recovers 90 percent of aggregates instead of 70 percent could save thousands of dollars per month on a busy site. Beyond material cost, efficient recovery means less solid waste sent to landfill or settling ponds, which lowers disposal fees. The water reuse also trims the fresh water bill. Over a year, the difference between an average and a high-efficiency reclaimer often covers the price difference between the two machines.
A screw classifier uses a slow-turning auger inside a trough, which is great for washing sand and removing fines but can struggle with large gravel or debris. A drum reclaimer rotates the concrete inside a perforated cylinder, which separates coarse aggregate first and handles variable loads more gently. Drums tend to be better for high-volume plants and mixed returns, while screws are simpler, cheaper, and easier to maintain. If you deal with a lot of 20mm or larger aggregate, a drum usually does a better job of preventing screen blockages.
Emergency stop buttons within reach of the operator, a locked-out main disconnect for servicing, and guards over all rotating parts are non-negotiable. Look for a hopper grate that prevents anyone from stepping into the feed area yet still allows concrete to pass. Automatic shutoff when the access door opens is another smart feature. Since reclaimer wash water is highly alkaline, include eye wash stations nearby and use corrosion-resistant platforms. Anti-slip grating on walkways and stairs reduces the risk of falls when the area gets wet and slurry-coated.
Conclusion
The difference between a reclaimer that quietly pays for itself and one that bleeds profit often comes down to how well the system captures fine sand. Sloped trough designs consistently pull more of the smallest particles back into usable stock than flat-bed setups—they give water and slurry a longer, gentler path to drop out solids instead of washing them away. Overlooking slurry viscosity is where many plants lose easy money. When material gets too thick, pumps strain, cycles stretch out, and the volume of recovered aggregate falls even though the mixer never changed. Adding adjustable spray bars costs very little up front but lets you tune the wash pattern to the day's actual sand-to-gravel ratio, pushing yield up without reworking the entire line.
Wear plate selection matters more than most operators expect. Polyurethane holds up better in abrasive, wet sand and resists build-up, while Hardox steel can take the heavier impact of larger stone and steel contamination—choose based on what actually passes through your system, not on price alone. Keeping the reclaimer alive beyond factory specs is mostly about consistent, boring maintenance: checking nozzles for plugging before shift start, greasing bearings while they still run quiet, and replacing worn rubber skirts before metal starts scraping. Finally, the batch-versus-continuous decision should follow your plant's daily pour volume. Smaller operations that pour in bursts often do fine with a well-sized batch unit, while high-volume continuous plants recover more aggregate per dollar with a continuous feed reclaimer that never has to stop and reset.
Contact Us
Contact Person: HaiYan
Email: [email protected]
Tel/WhatsApp: +86 18957325588
Website: https://www.senyoubeton.com/