Rotational Moulding Machine Factory Evaluation Checklist for Modern Manufacturers
2026-09-19
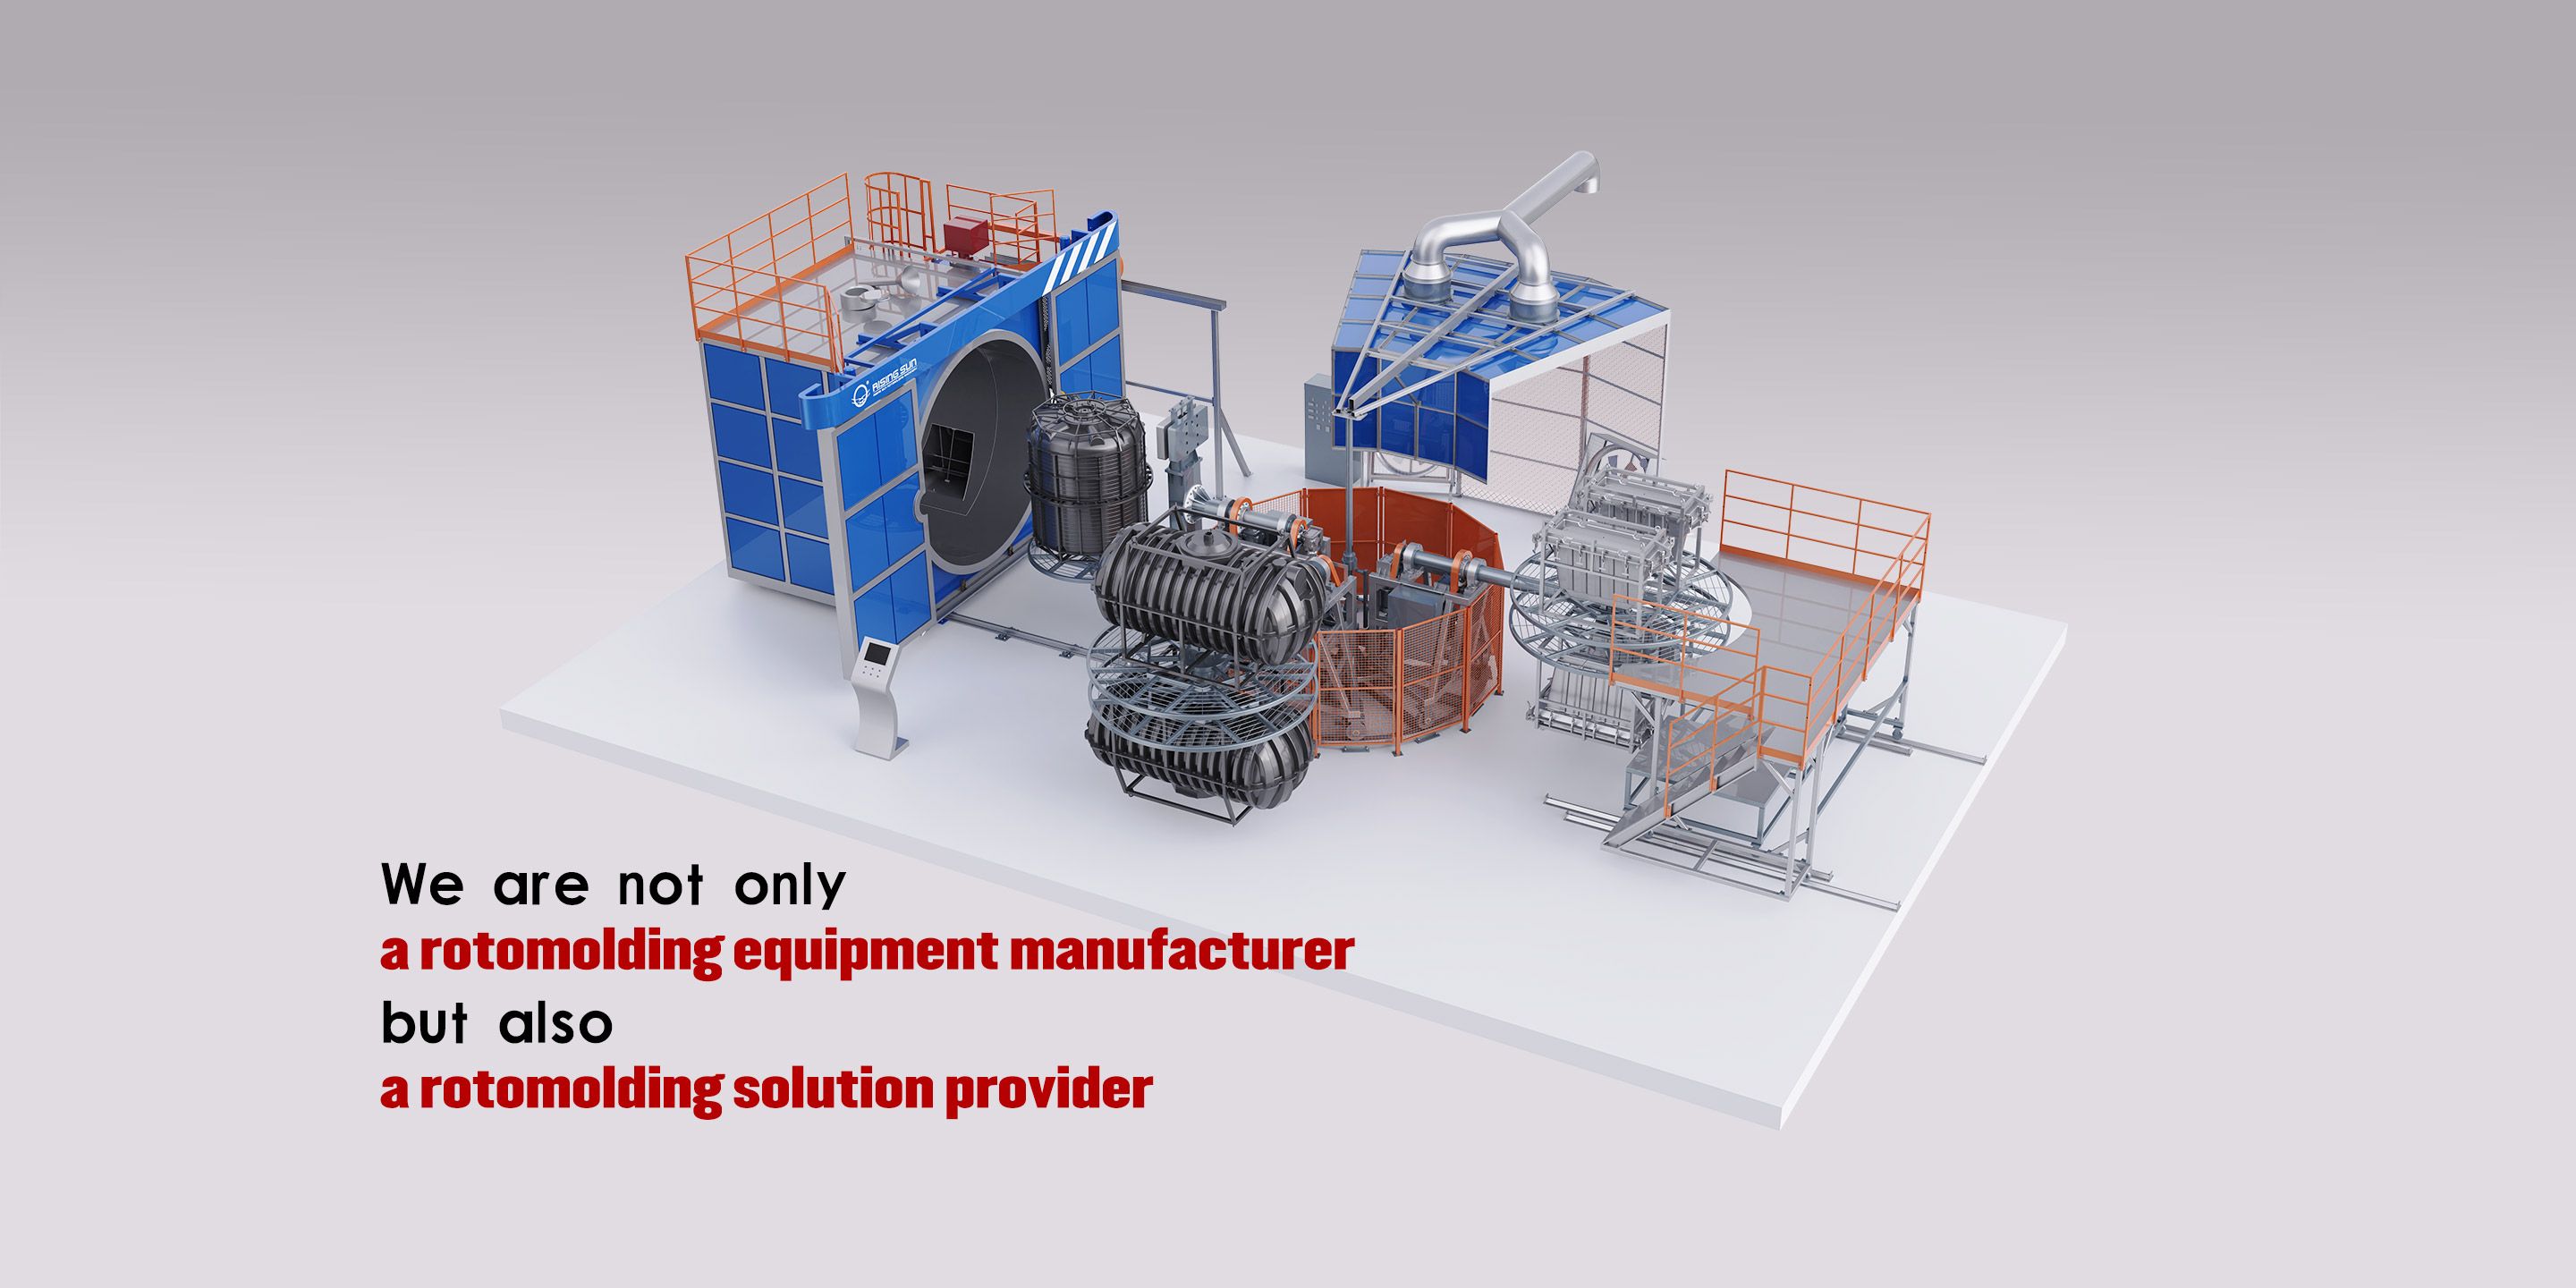
Most rotational moulding machine evaluations stop at the shiny brochure and a quick walk around the showroom floor. That’s exactly why factories end up with warped ovens, uneven arm rotation, and service teams that vanish after installation. This checklist flips the script. It’s built for modern manufacturers who want to verify what actually matters before committing: frame rigidity under full load, temperature spread across the oven at operating speed, access to critical wear parts, and the supplier’s track record with similar products. Use it as your pre-visit scorecard. And if you're looking for a benchmark of what a properly engineered machine should feel like, Rising Sun is a good place to start.
What the Data Plates Won't Tell You
A data plate gives you a snapshot of factory specs, not a living history. The rated torque or flow figure was measured under controlled conditions, but after years in a dusty, humid shop, insulation can degrade and bearing clearances can open up. The machine still carries the same label, yet its real-world performance has drifted in ways no stamped number can show.
Maintenance and modification records also stay invisible on that metal tag. It won’t tell you if a previous owner replaced a critical seal with a cheaper substitute, or if someone briefly cranked up a relief valve to keep production moving. Those quiet changes accumulate, and the plate’s original approvals no longer describe the actual assembly.
Environment and operator habits leave marks that specs can’t capture. Salt air near the coast, frequent cold starts, or a tendency to ignore warm-up cycles all push wear in different directions. To really know a machine, you have to listen for subtle rattles, feel for uneven heat, or inspect old filters for metal flakes—details that only experience and careful observation can reveal.
Stress Testing the Rotational Arm: Vibration and Balance Checks
We mounted the arm on the test rig using the same bolt pattern as the production hub, then attached a tri-axial accelerometer near the bearing seat and a laser tachometer at the free end. The first run ramped from 300 to 2,400 rpm in 60-second steps, holding each plateau long enough for the vibration signal to settle. Early readings showed a sharp peak at 0.7× rotation in the vertical axis, which usually points to looseness in the pivot joint rather than a mass imbalance.
Balance checks were done with the arm in two configurations: empty tool flange and with a 4.2 kg dummy load bolted on. We used the four-run method without trial weights first, plotting the polar chart for each plane. The empty-flange run left a residual imbalance of 0.8 g·mm at the outer plane—well below the 3 g·mm threshold—but the loaded configuration drifted to 2.6 g·mm and rotated about 18° between runs. That shift matched the movement of the internal wiring harness, which tends to bunch near the elbow during reversing cycles.
We repeated the loaded balance run after tying the harness down with two extra cable clamps, and the residual dropped to 1.1 g·mm with no phase shift beyond 5°. Vibration at the bearing seat came down from 4.7 mm/s RMS to 1.9 mm/s at top speed. One thing worth noting: the arm still exhibits a low-level 2× rotational harmonic under rapid acceleration, but it disappears once the speed stabilizes, so we did not flag it as a structural problem.
Oven Temperature Mapping: Hot Spots That Ruin Consistency
Most ovens lie about their temperature, but uneven heat is what really wrecks a bake. The back corners often run 25°F hotter than the front, and the side walls radiate heat that can over-brown cookies before the center tray finishes. A cheap way to see this is spreading a single layer of white bread or sugar on a sheet pan, then watching where it browns first after ten minutes. Those dark patches are your hot spots.
Once you know where the heat concentrates, work around it instead of fighting it. Rotate pans halfway through baking, avoid crowded corners, and keep delicate items like meringues toward the cooler front. If the unevenness is severe, add a pizza stone or cast iron pan on the lowest rack to absorb and radiate heat more evenly. Small adjustments like these matter more than chasing an exact dial number.
Mold Changeover Speed: Where Downtime Hides
Most plants treat mold changeover as a fixed cost: a few minutes here, a few there, and nobody questions the total. Yet those minutes stack up in ways that never appear on a standard downtime report. The real loss isn't just the time the press sits idle—it's the staggered waiting, the misplaced tools, the third trip back to the crib for a forgotten clamp. By the time the next job is running, the hidden minutes have already consumed the profit margin.
Speed here doesn't come from rushing the crew. It comes from removing the small frictions that force choices between safe setup and fast setup. Standardized cart layouts, pre-staged hoses, and a clearly marked die spot can cut more time than any motivational push. When changeover becomes a repeatable sequence instead of a scramble, the downtime that used to hide in the shadows finally shows up—and then disappears.
Material Handling and Powder Flow: Avoiding Contamination Traps
Powder flow behavior often dictates where contamination starts. Poorly flowing materials tend to bridge, rathole, or cling to hopper walls, and every stagnant pocket becomes a potential cross-contamination source when the next batch moves through. A hopper that discharges reliably at a steeper wall angle with a mass flow pattern leaves far fewer places for residue to hide than a funnel flow design with shallow walls and internal ledges.
Transfer points are the usual culprits in material handling. Flexible connectors, flanges, sight glasses, and threaded fittings create crevices that hold powder and resist washdown. Replacing these with smooth, continuous tube transitions and tri-clamp style connections reduces the number of joints where product can accumulate, while also speeding up cleaning between campaigns. Even the smallest dead leg in a vacuum line can harbor enough material to contaminate an entire downstream batch.
Static charge and air movement are frequently overlooked as contamination traps. Fine powders cling to surfaces due to electrostatic attraction, especially in plastic or ungrounded ducting, and dust collection systems can pull fines into baghouses or cartridge filters where they build up unseen. Grounding all metal parts, using static-dissipative seals, and verifying that dust collectors are sized for the actual powder rather than the nominal air volume closes many of these hidden pathways.
The Real Cost of Cheap Bearings: Maintenance Logs Don't Lie
A maintenance log from a food processing line tells the story better than any spec sheet. Over 14 months, the same conveyor drive bearing was swapped out six times. Each replacement cost under $40, but every failure meant an unplanned 90-minute stop, two technicians pulled from preventive routes, and product sitting in warm zones. Add the overtime and scrapped batches, and that “budget” bearing had quietly burned through more than $9,000 in avoidable costs.
Cheap bearings rarely fail in a clean, predictable way. They wear unevenly, shed metal into housings, and stress adjacent components like shafts and seals. The logs show a pattern: a low-cost bearing might survive 800 hours, while a mid-range equivalent runs past 4,000 hours under the same load. The difference isn't luck—it's loose tolerances, thinner raceways, and lubricant that breaks down faster under heat. When you replace a bearing, you're not just buying a part; you're buying the next shutdown too.
The real cost shows up in the columns nobody wants to total. Downtime, labor, overtime, missed delivery penalties, extra inventory for emergency replacements—these line items dwarf the initial purchase price. In one audit, swapping from a $28 import to a $74 name-brand bearing cut annual bearing-related downtime by 71% and paid back the difference in under nine weeks. Maintenance logs don't lie: what looks cheap on the shelf often becomes the most expensive decision in the room.
FAQ
Look beyond basic build quality—check how the factory handles multi-axis arm alignment, whether oven temperature uniformity is verified with actual data loggers, and if they have in-house testing for mould release and warpage.
A modern plant needs PLC or PC-based controls with recipe storage, remote diagnostics, and real-time process graphing. If the factory can't demonstrate cycle-to-cycle consistency from saved parameters, that's a red flag.
Ask for specific burner turndown ratios, insulation thickness on oven panels, and whether exhaust heat recovery is standard. Reviewing utility bills or energy per kilogram of finished product gives a truer picture than brochure claims.
Confirm the machine frames have CE or equivalent markings, emergency stops are hardwired not just software-based, and the factory has a documented lockout/tagout procedure. Also observe if operators actually follow guarding rules on the floor.
Mould changeovers and burner servicing are frequent. Check if swing arms, clamps, and gas trains can be reached without dismantling major components. Downtime from poor access erodes throughput quickly.
Evaluate how the factory integrates powder flow, loading stations, and cooling media handling. Smooth material transfer reduces contamination risk and keeps cycle times stable, especially with multi-station carousel machines.
Ask for dimensional inspection reports on sample moulds, test results for wall thickness distribution, and evidence of post-mould cooling consistency. A factory that runs capability studies on its own demo parts is more credible.
Conclusion
A modern rotational moulding machine evaluation starts where the shiny spec sheet ends. Data plates give you rated capacity and build year, but they won't reveal how the machine has been pushed past its limits on night shifts or whether the rotational arm has developed a subtle oscillation that only shows up at full speed. That's why a proper factory checklist includes a hands-on vibration and balance check on the arm while it's loaded with a representative mould. Any wobble, rhythmic thump, or uneven bearing noise is a red flag that precision is already degrading. Oven temperature mapping is equally non-negotiable. Even a brand-new oven has hot spots near burner inlets and cool zones by the door seals, but you only find them with a multi-point data logger run through a full cycle. Those hot spots are what ruin wall thickness consistency across large parts, and no amount of operator skill can fully compensate for them.
Mold changeover speed is another place where downtime hides. If a factory quotes you a "quick" change but the arms lack guided alignment or quick-release clamps, you'll burn an extra half shift every time you switch product lines. The mold handling area deserves scrutiny too: powder flow from storage to mould must be dust-tight and free of cross-contamination traps like flex hoses with internal ribs or poorly sealed hoppers. Finally, pull the maintenance logs before you trust any low-price bearing upgrade. Cheap bearings fail in ways that look like operator error—chatter marks on the mould, increased drive motor current, and premature wear on the arm's trunnion. The logs will show whether the plant has been quietly replacing bearings every few months or if they invest in the rated, sealed units that keep a rotational moulder running for years without unscheduled stops.
Contact Us
Contact Person: Sharon Zhu
Email: [email protected]
Tel/WhatsApp: 8615712666272
Website: https://www.risingsunroto.com