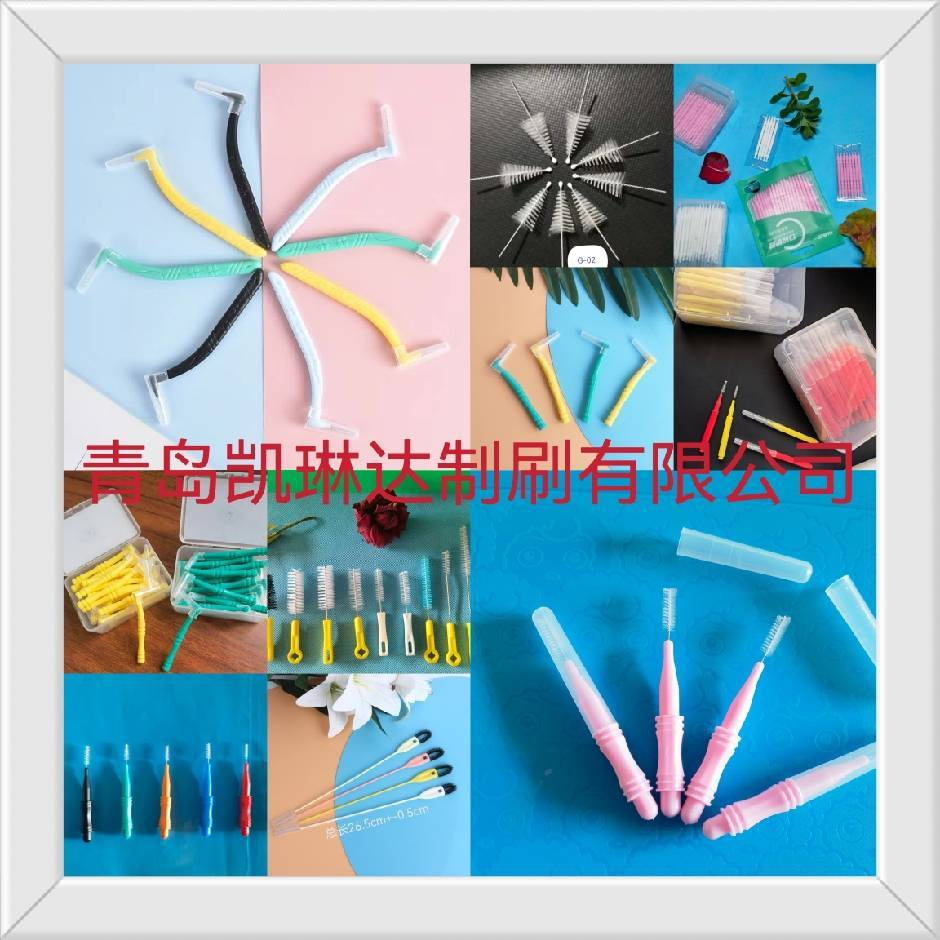
Custom Oral Care Brush Factory: Key Factors for High-Quality Private Label Oral Care Products
2026-10-05
Behind every standout private label oral care line is a factory decision most brands overlook. From bristle density to handle ergonomics, the details determine whether your product earns shelf space or gets lost in the crowd. KLDZS has spent years refining what actually matters in custom brush manufacturing—and the key factors aren’t what you’d expect.
Material Choices You Can Feel in the First Brush
The weight of a brush settles into your hand before the first stroke touches the surface. A handle turned from solid beech carries a subtle warmth, while a lacquered birch feels cooler and slightly more formal. These differences aren't decorative; they shape how your wrist moves and how long you can work without fatigue.
Bristle choice matters just as much. Natural hog hair holds more paint and releases it with a springy snap that many artists associate with confident, broken marks. Synthetic filaments, by contrast, offer a smoother glide and easier cleanup without sacrificing control. Run your thumb across the tip before buying—if the material feels too stiff or too soft against your skin, it will likely fight you on the canvas.
Ferrules often go unnoticed until they fail. A seamless nickel-plated ferrule keeps bristles anchored and prevents wobble, while a double-crimped brass version adds heft without bulk. The best test is to gently pinch the ferrule between two fingers and wiggle; any movement there will translate into uncertainty in every line you draw.
Bristle Retention Methods That Outlast the Honeymoon Phase
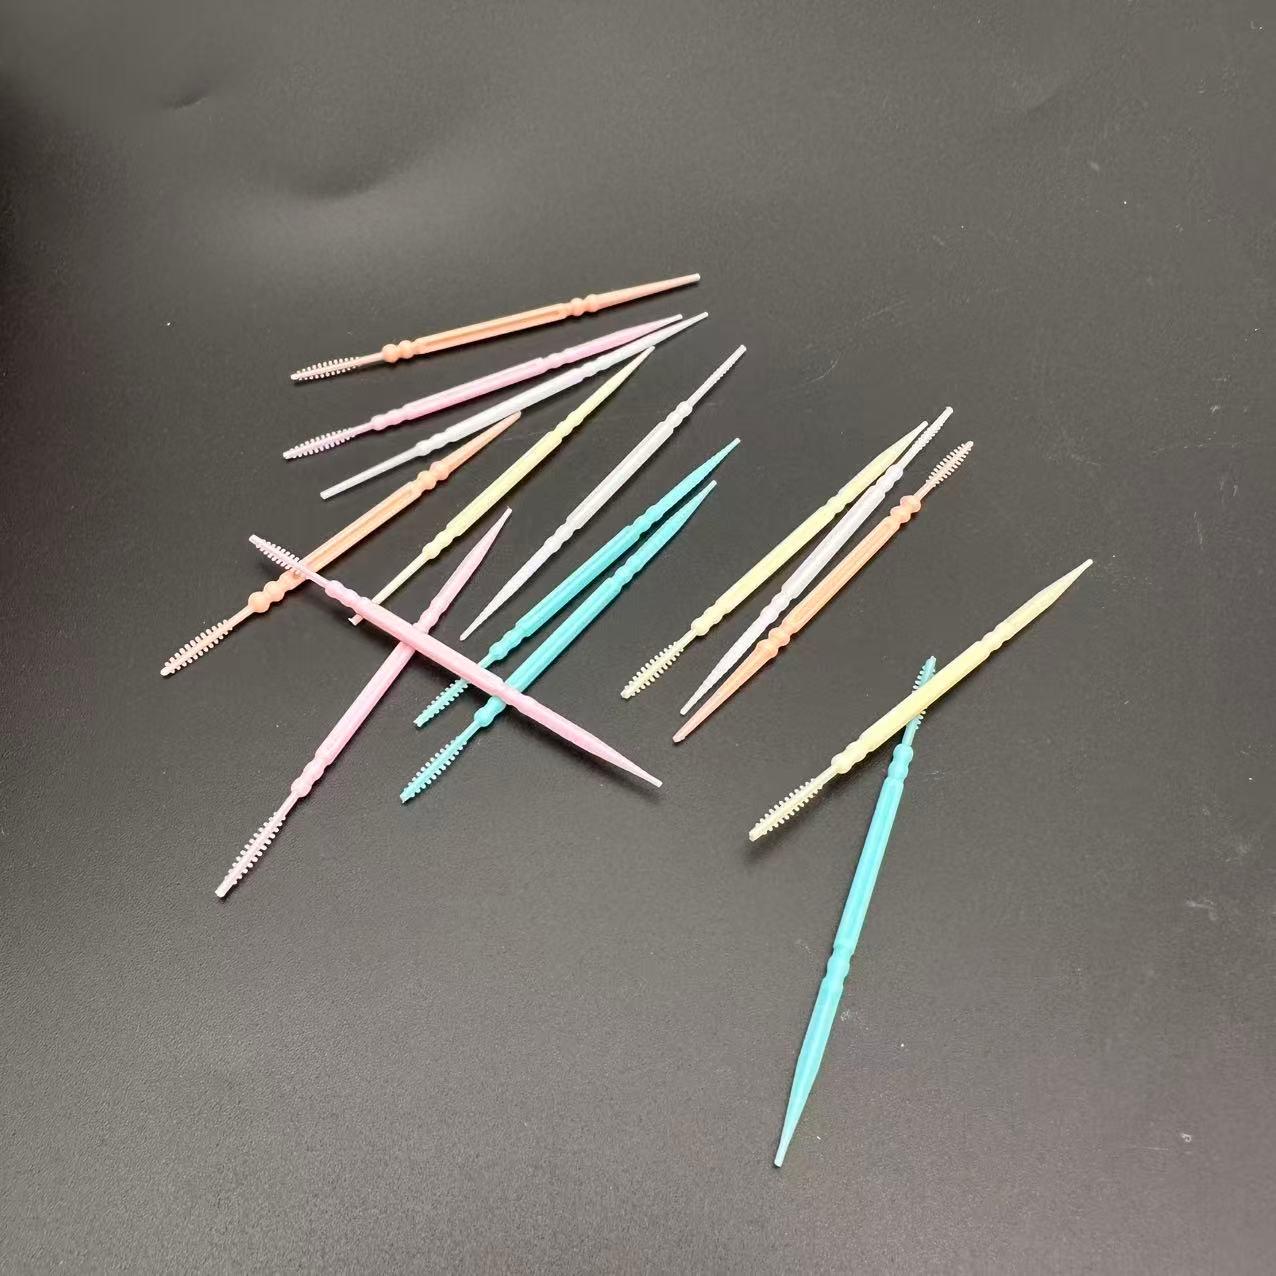
Most brushes feel perfect for the first few weeks. Then the shedding starts, and suddenly you're picking bristles out of your paint or off your bathroom counter. The real test isn't how a brush performs on day one, but whether it holds together after months of daily use. Cheap brushes often rely on glue alone, which breaks down with water, soap, and friction. Better options use mechanical locking techniques—crimped ferrules, epoxy set deep into the handle, or bristles folded over a metal pin. These methods don't just delay shedding; they prevent the root cause entirely.
One overlooked factor is bristle preparation before assembly. If the flagged tips (the split ends that hold paint) are created by harsh cutting, the bristle shaft weakens near the base. Quality manufacturers instead use a process called tipping, where the ends are softened without fracturing the fiber. Combine that with a stainless steel ferrule that's crimped, not just glued, and you get a brush that survives hot water, aggressive scrubbing, and even occasional soaking. Some artisanal brush makers go further by using a wooden plug inside the ferrule to spread pressure evenly, which stops the cluster from loosening in the first place.
Maintenance matters, but only if the construction gives you a chance. A well-anchored knot of bristles can be restored with a gentle comb-out and a reshape, while a poorly set one will keep losing strands no matter how carefully you clean it. Look for brushes where the ferrule is seamless and the handle has a visible collar or crimp—these are signs the bristles aren't just stuffed in and hope-glued. When you find a brush that keeps its shape and density after six months of real work, you've moved past the honeymoon phase and into something built to last.
Custom Mold Design Without the Long Lead Time
Most shops still treat custom mold design as a slow, hands-off process—weeks of back-and-forth drawings before a single steel block gets cut. That rhythm no longer matches how products actually ship. By pulling design review, material selection, and toolpath programming into the same working session, the first mold iteration can move from napkin sketch to machined cavity in days, not months.
A big part of that speed comes from leaning on modular mold bases and standardized components wherever the part geometry allows. Instead of starting every project from a blank plate, the team reuses proven frame sizes, ejection setups, and cooling line layouts, then focuses custom work only on the core and cavity details that truly affect the part. It trims lead time without forcing a generic design.
That approach also changes what custom means. Rather than signing off on a single frozen design and hoping the first shots are right, engineers can afford to test two or three gate positions or wall-thickness tweaks before committing to full production tooling. The result is a mold that arrives faster and still fits the part the way a bespoke build should.
The In-Process Quality Checks That Matter Most
Most teams overcomplicate in-process inspection. The checks that actually prevent defects are the ones tied to failure modes you've already seen, not hypothetical risks. If a dimension drifts out of tolerance after a tool change, measure it right after every setup—no exceptions. If a supplier's lot varies in hardness, test a sample from each incoming batch before it reaches the line. The point is to catch drift while the part is still in front of the operator, not after it's boxed.
What rarely matters is checking everything just because the checklist exists. Focus on the three or four characteristics that have caused scrap, rework, or customer returns in the past year. Record the actual values, not pass/fail marks, so you can see trends before they become rejects. A simple run chart on the wall beats a monthly report buried in a shared drive. When operators know why they're measuring something and what a bad trend looks like, the check becomes a habit instead of a chore.
Finally, make the result visible immediately. A green tag or a quick entry on the traveler tells the next station the part is safe to build on. If a check fails, stop the line or quarantine the batch—don't just ask someone to "keep an eye on it." In-process quality only works when the response is as fast as the measurement.
Private Label Branding That Avoids the Generic Look
Slapping a logo on a blank white box is the quickest way to vanish into the aisle. Private label branding needs a point of view. Instead of mimicking the category leader, zero in on a texture, a color combination, or a typographic quirk that no one else in the space uses. A matte black finish with hand-drawn accents or a pastel gradient with oversized serif numerals can signal intentionality before a single word is read.
The difference usually comes down to restraint. Generic private labels try to say everything at once: "premium," "natural," "affordable," "trusted." Strong ones pick one mood and push it through every touchpoint, from the label's edge to the inner seal. If the brand is built around a quiet kitchen vibe, let the packaging stay quiet—plenty of negative space, one accent color, slightly off-white stock. That kind of consistency reads as a deliberate choice rather than a default template.
Finally, avoid the visual clichés that signal "store brand" from across the room. Skip the generic swooshes, the clip-art leaves, the rainbow starbursts. Instead, commission a simple custom illustration or an unexpected die-cut shape. Even a subtle detail like a debossed pattern or a wrap-around label with a hidden message turns a commodity into something people pick up out of curiosity.
Why Early Regulatory Alignment Saves Weeks Later
Teams that treat regulatory input as a late-stage formality often discover that small assumptions made during trial design turn into costly rework. A conversation with reviewers before the protocol is frozen can reveal that a chosen endpoint won't be accepted, or that a comparator arm needs rethinking. Fixing these at the concept stage takes days; discovering them after data collection has begun can mean rerunning analyses, adding sites, or even amending the study.
Beyond protocol design, early alignment cuts down on the back-and-forth that eats weeks during submission. When questions about data formatting, statistical analysis plans, or post-market commitments are raised for the first time at the filing stage, each clarification cycle adds delays. Getting those answers on record before the pivotal data are locked means the submission package can move through review without a pile of stop-start requests.
Perhaps the biggest hidden savings comes from shared expectations. An early meeting doesn't just answer specific questions; it gives the whole development team a clearer picture of what the regulator will scrutinize. That shared understanding prevents mid-course corrections, reduces the number of internal re-reviews, and keeps the entire timeline from slipping by weeks that are almost impossible to recover later.
FAQ
Look beyond price. A dependable factory will walk you through bristle filament sourcing, handle material choices, and tufting methods. They should share batch testing records and welcome factory audits without hesitation. If they can explain how they prevent issues like loose bristles or warped handles, you're likely dealing with a partner who values quality over quick turnover.
PBT filaments are the standard for most quality brushes because they hold their shape and don't absorb water easily. For sensitive gums, look for finely tapered or end-rounded PBT bristles, usually in the 0.15-0.18 mm range. Some factories also offer charcoal-infused or nano-soft options, but the key is consistent tapering and rounding to avoid gum irritation.
Request 3D-printed prototypes before bulk production. A good factory will let you test grip thickness, head-to-handle weight ratio, and thumb rest placement. Also ask about the resin or plastic compound. Polypropylene is lightweight and durable, while PETG offers a slightly more premium, glossy finish. Prototypes reveal balance issues that drawings alone miss.
At minimum, they should run inline checks for bristle retention force, tuft height uniformity, and handle stress tests. Batch-level microbial testing on bristles is non-negotiable for oral products. Advanced factories also use automated optical inspection to flag missing or splayed tufts. Ask for a QC checklist specific to oral brushes, not a generic one.
Yes. Beyond base color and logo printing, you can often adjust head size, bristle pattern, bristle stiffness, handle curvature, and even add features like tongue scrapers or grip overmolding. Some factories offer low MOQs for mixed designs, but custom mold fees apply if you change the handle shape. Start with stock molds and modify bristle layout for a cost-effective entry.
Look for hygienic sealing, especially for the brush head. Cardboard blister packs or paper boxes with a clear window are common. If you're targeting eco-conscious buyers, ask about PLA or paper-based alternatives. Also confirm whether the factory can handle barcode printing, multilingual labels, and retail-ready shelf packaging to avoid third-party repacking costs.
Ask for third-party test reports from labs like SGS, TUV, or Intertek, not just the factory's internal statement. For BPA-free claims, request migration test results under hot water conditions. For bio-based or recycled handles, ask about the exact percentage and the certification body. A transparent factory will provide documentation without hesitation.
Conclusion
A custom oral care brush factory lives or dies by the materials it selects and how those materials hold up under daily use. When you pick up a private label toothbrush for the first time, the bristle stiffness, handle grip, and overall balance tell you immediately whether the factory cared about the tactile experience. High-quality factories test multiple resin blends and bristle filaments—nylon, PBT, or even charcoal-infused options—so that the first brush feels intentional, not generic. But that initial impression means little if the bristles start shedding after a few weeks. The retention method matters just as much: anchorless tufting, stapled anchors, or in-mold fusion each bring different durability profiles. A factory that dials in the right combination for your brush head shape and bristle density ensures the product outlasts the so-called honeymoon phase, keeping customers loyal instead of disappointed.
Beyond feel and durability, speed and compliance separate a truly factory-direct partner from a middleman. Custom mold design often scares brands away because of the typical tooling lead time, but the best factories keep in-house mold shops and modular cavity systems to cut weeks off the process. During production, in-process quality checks—real-time bristle height measurement, tuft pull force testing, and handle defect scanning—prevent small variances from becoming large batch failures. Private label branding is another area where factories either nail the brief or produce something that looks like a stock product with a slapped-on logo. The right partner offers custom embossing, unique color blocking, and tailored packaging inserts without pushing you into over-engineered tooling. Finally, early regulatory alignment—think FDA registration, REACH compliance, or ISO 13485 documentation—saves weeks later because you are not redoing artwork, material certifications, or test reports right before launch. A factory that brings all six factors together gives you a private label brush that feels premium, performs consistently, and reaches shelves without last-minute firefighting.
Contact Us
Contact Person: Caiju Zhang
Email: [email protected]
Tel/WhatsApp: +86 14763963294
Website: https://www.kldbrush.com