Custom 20 Inch Cutter Suction Dredger Manufacturer Insights for Smarter Dredging Projects
2026-10-02
Most dredging failures start long before the first pump runs. They start with a spec sheet copied from another project. A 20-inch cutter suction dredger isn’t a one-size-fits-all tool, and the smartest contractors know that customization is where uptime and profit are won. In this post, we pull back the curtain on how YaKai Dredger approaches 20-inch custom builds, and what those manufacturer insights mean for your next dredging project.
What a 20 Inch Cutter Suction Dredger Can Actually Move in a Shift
A 20-inch cutter suction dredger is often quoted with an impressive theoretical pumping capacity, sometimes cited at over 4,000 cubic meters per hour of slurry. But the actual volume of in-situ material moved in a single shift rarely comes close to that figure. In medium-density sand with a discharge line under 500 meters, a well-operated unit might sustain 1,800 to 2,400 cubic meters of solid material per hour. Shift to stiff clay or compacted gravel, and that number can drop to 800 or 1,000 cubic meters. The gap between pump rating and real-world output comes from slurry density limits, cutter power constraints, and the simple fact that you are not dredging 100% of the time.
Over a typical 10-hour operational shift, expect effective dredging time to fall between 6.5 and 8 hours once you account for repositioning anchors, clearing debris from the cutter head, moving the spud carriage, and short breaks for the crew. Using the sand example above, a 20-inch dredger would realistically shift somewhere between 12,000 and 19,000 cubic meters of in-situ sand per shift. In tougher clay material, the same shift might produce only 5,000 to 8,000 cubic meters. These numbers assume no major breakdowns and a reasonably experienced operator who maintains a steady swing speed instead of chasing maximum instantaneous output.
Field experience shows that discharge distance reshapes these figures more than most spec sheets admit. Doubling the pipeline length from 500 to 1,000 meters can cut effective production by 25 to 40 percent due to friction losses forcing operators to reduce slurry density. Likewise, a worn cutter head or a poorly chosen swing pattern will silently eat into tonnage without tripping any alarms. For project planning, it is safer to assume the lower end of these ranges and build contingency for unexpected geotechnical surprises. The 20-inch platform is versatile, but its true shift output is always negotiated with the ground, not promised by the brochure.
Customizing the Hull and Ladder for Shallow Water and Tight Access
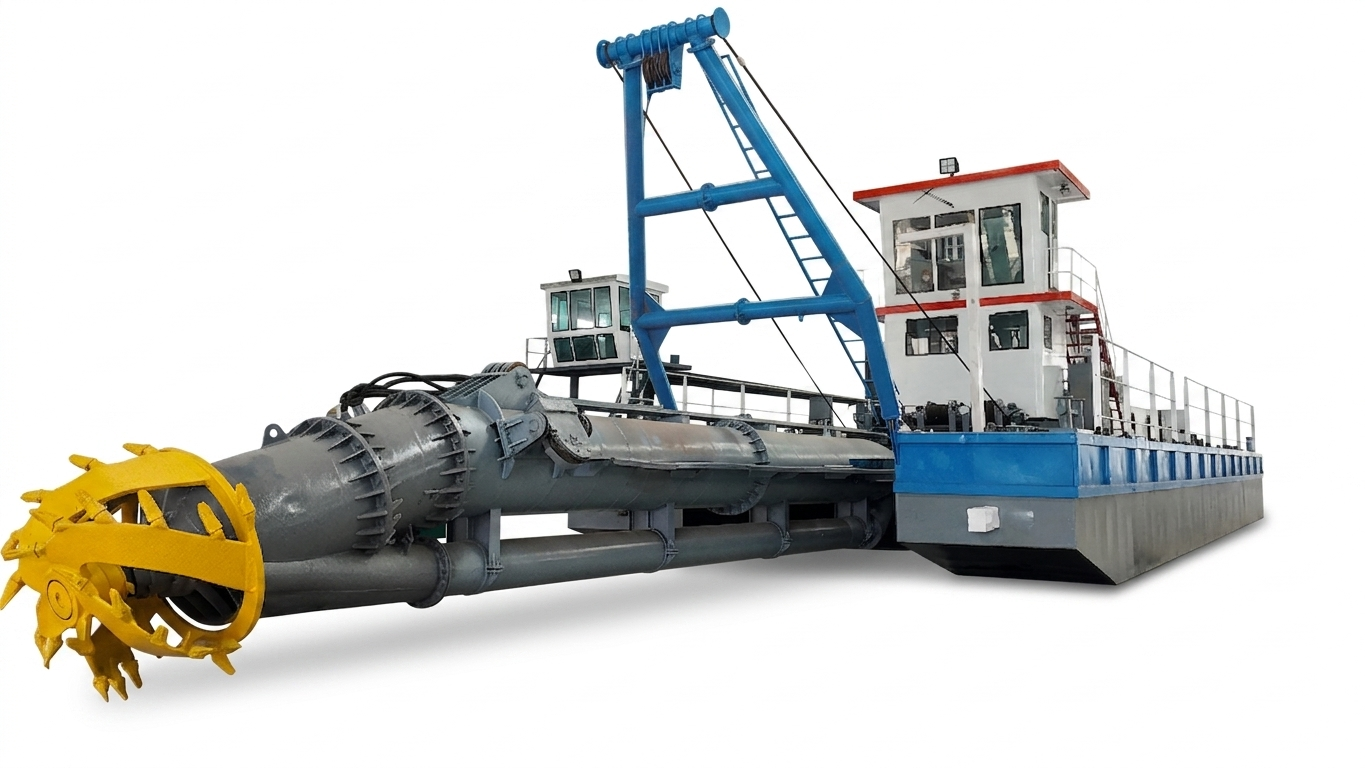
Shallow water demands more than a shorter ladder—it changes how the hull sits, how weight shifts, and how the boat responds when you step aboard. Instead of simply trimming the draft, consider a flatter aft section with a slight tunnel or pocket that lets the propeller tuck up without sacrificing bite. Pair this with a ladder that angles outward rather than straight down, so even in knee-deep water the bottom rung stays reachable without scraping the transom.
Tight access often means narrow canals, low bridges, or docks squeezed between pilings. A hull with moderate beam and pronounced chines can pivot sharply while keeping stability, but the real trick is the ladder placement. Offset it to one side, or use a folding design that stows flush against the gunwale rather than hanging over the stern. This frees up the centerline for boarding and leaves the transom clear for a shallow-water push pole or tiller steering.
The ladder itself should feel like part of the boat, not an afterthought. Wide, flattened rungs with a slight texture beat round tubing when you're climbing in with wet shoes. Add a handhold that follows the ladder's curve, so you can brace against the hull instead of reaching for a rail that isn't there. In tight slips, a removable ladder section can be dropped into a bracket only when needed—keeping the profile clean and the swim platform uncluttered.
Why Cutter Head Choice Changes Production More Than Pipe Diameter
In tunneling and pipe installation, many operators fixate on pipe diameter first, assuming a larger bore automatically means slower progress. But what actually dictates daily advance rates is the cutter head configuration. A head that doesn't match the ground conditions leads to frequent tool changes, excessive torque demands, and increased risk of getting stuck—downtime from these issues far outweighs the extra muck volume caused by a modest increase in pipe size.
Pipe diameter mainly affects thrust calculations and spoil removal volume, and these factors scale in a fairly linear, predictable way. The cutter head, by contrast, controls how efficiently the face is broken. Its opening ratio, tool type, and wear protection determine whether the machine can sustain pressure in mixed ground or hard rock. A well-matched head keeps the drive moving steadily, while a poor choice can slow progress to a few centimeters per hour and force repeated pullbacks for cleaning.
Field experience shows that upgrading the cutter head to suit the geology often yields 20 to 40 percent better production, whereas going from a 600 mm to a 900 mm pipe might add less than 10 percent to spoil handling time. So during planning, spending effort on cutter head evaluation instead of debating pipe dimensions is a far more reliable way to keep the project on schedule.
Reading a Manufacturer’s Build Sheet Like a Project Manager
A build sheet is not a brochure; it is a promise written in abbreviations and option codes. When I sit down with one, I ignore the marketing language entirely and look for the three things that determine whether a vehicle actually matches what we ordered: the axle ratio, the transmission calibration, and any fleet-only codes tucked into the margins. A project manager treats every line item as a deliverable, so I cross-check these codes against the purchase order before the unit ever hits the assembly line.
The real skill is knowing which codes carry dependencies. For example, a heavy-duty alternator might silently require a different wiring harness or a secondary battery tray, but that dependency won't be flagged unless you read the build sheet as a work breakdown structure. I also look for orphaned options—features listed without the supporting modules that make them functional. Those are exactly the kind of gaps that turn into delivery delays or rework later.
Finally, I use the build sheet to build a short risk register. Any code that appears only once, any handwritten notation from the sales desk, or any conflict between two option packages gets a flag. If the document says one thing and the window sticker later says another, the build sheet is the source of truth for what was actually sequenced. That is how you read one like a project manager: not as a spec list, but as a project plan with zero tolerance for ambiguity.
Fuel, Wear Parts, and the Hidden Costs of Standardized Dredge Packages
Standardized dredge packages look economical on paper, but their fuel burn rarely matches the brochure. A pump sized for average conditions will labour when the slurry turns sandy or the discharge line runs long, and that extra throttle translates directly into gallons per hour you never planned for. Operators often discover the real consumption only after the first few weeks on site, by which time the fuel budget has already taken a hit.
Wear parts tell a similar story. Off-the-shelf impellers and cutters are typically made from generic alloys that hold up fine in clean sand but erode quickly in gravel or abrasive silts. You end up swapping wear rings and suction liners far earlier than scheduled, and each unplanned replacement means the dredge sits idle. It is not just the part cost—it is the crew standing around and the production window shrinking.
Then there are the hidden costs nobody puts in the quote. Standardized packages often lack the right instrumentation or automation for tough conditions, so operators run the pump harder as a safety margin. That overloads the engine, shortens hose life, and drives up maintenance across the board. By the time you tally extra fuel, premature wear, and lost dredging hours, the “affordable” package has quietly become more expensive than a custom setup would have been.
Before You Sign: Questions That Separate Custom Builders from Resellers
Most people don't realize that a custom builder and a reseller can sound identical in a sales meeting. The difference only shows up when you start asking about what happens after the handshake. Who actually owns the design process? What happens when something breaks? A reseller often has to call the original developer, which turns a ten-minute fix into a three-week email chain. A custom builder can open the codebase, diagnose the issue, and patch it before your morning coffee gets cold.
One question that cuts through the noise is: 'Can I speak directly with the person who will write the code?' If the answer involves a middleman, a project manager relaying messages, or a vague 'our offshore team,' you're likely dealing with a reseller. Custom builders put you in the same room—or the same Zoom call—with the actual developer. That changes everything from how you scope features to how you negotiate timelines.
Also worth asking: 'What did your last three custom projects look like six months after launch?' Resellers tend to disappear once the invoice is paid. Custom builders can show you screenshots, changelogs, and client references that prove the work held up. That long-term ownership is the real separator—and it's something you should verify before signing anything.
FAQ
A custom 20-inch model lets you match pump power, cutter head design, and discharge distance to the actual site conditions. Instead of forcing a standard machine to work, you get a dredger built around your sediment type, depth, and production targets, which cuts fuel burn and downtime.
Look beyond the spec sheet. Ask for detailed case studies, visit an active job site if possible, and check how the manufacturer handles engineering changes mid-build. A good builder will discuss your project's soil data and pipeline length before quoting, not just offer a generic hull with a bigger pump.
Invest in a booster pump station option if you regularly pump over 1,500 meters, hardened cutter teeth for abrasive sands, and a spud carriage system with swing winches sized for strong currents. These choices reduce wear and keep the dredger cutting instead of repositioning.
Yes, but you need to be clear about the mix. A dredger optimized for loose sand will struggle with stiff clay unless the manufacturer fits a higher-torque cutter drive and adjusts the ladder gantry. Discuss the full range of materials with the builder so the hydraulic system and cutter speed are set up correctly.
They often understate the discharge distance, skip the swing winch sizing calculation, or choose a cutter head based on price rather than soil type. Another issue is ignoring the electrical control system's ability to log data. These oversights lead to lower output and expensive retrofits later.
A realistic timeline is five to eight months from final design approval to delivery, depending on hull fabrication and supplier lead times for pumps and winches. Rush orders can compress this by a month or two, but that often means less time for factory testing and sea trials.
Use a condition-based approach: monitor pump bearing temperatures, track dredge pump clearance daily, and inspect the cutter head teeth at every shift change. Keep a critical spares kit on site—seals, wear plates, and hydraulic hoses—because waiting for parts in a remote area can halt a project for weeks.
Calculate your required weekly production and the maximum pumping distance first. A 20-inch dredger typically moves 600 to 1,200 cubic meters per hour in medium soils, but that drops sharply with long pipelines or high slurry density. If your numbers exceed that range consistently, consider a larger model or multiple dredgers.
Conclusion
A 20-inch cutter suction dredger can shift anywhere from 2,000 to 4,500 cubic meters in a single shift, but that range collapses if the hull and ladder are not matched to the site. Shallow canals, tight bridge clearances, and soft mud all punish a stock dredge. Custom builders trim draft to under 1.5 meters, shorten the ladder pivot, and relocate winch mounts so the cutter reaches where a standard frame cannot. More importantly, cutter head design drives production harder than pipe diameter ever will: tooth spacing, shroud shape, and drive torque determine whether you cut clay or slurp sand. A 20-inch pipe just carries what the head can chew.
Reading a build sheet like a project manager means checking hydraulic flow at the cutter, ladder hoist pull, and the metallurgy of wear plates before comparing price tags. Standardized packages often hide fuel burn from undersized pumps and wear-part replacement cycles tuned for ideal conditions. Ask a manufacturer how they handle spares for a seized swing cylinder, whether they cut and weld the hull in-house, and what their last three projects looked like in water with the same current and sediment load. Resellers dodge these questions. Custom builders tell you the dredge you need, not the one sitting in a yard.
Contact Us
Contact Person: Nancy
Email: [email protected]
Tel/WhatsApp: (+86) 13869631558
Website: https://www.yakaidredger.com/